
Why Choose An ECA Generator


Solutions For Your Industry
-
-

Greenhouses
Irrigation line treatment, foliar spray, disease prevention — organic-certified
-

-
Water Bottling
Produce mineral-rich, alkaline ionized water; integrates easily into existing lines


Ready to get off chemical supply chains?
Talk to an OmniLyte specialist. We'll assess your flow rate needs, application, and recommend the right system — no obligation.

What Is Electrolyzed Water?
1. Salt + water in
The generator takes a dilute salt (NaCl) brine solution and tap water as its only inputs. No raw chlorine, no hazardous chemicals to handle or store.
2. Electrolysis on demand
Electrochemical activation (ECA) splits the solution into two powerful outputs:
- Anolyte: a disinfectant containing hypochlorous acid (HOCl), which many studies show is effective against bacteria, viruses, fungi, and biofilms.
- Catholyte: a gentle, alkaline cleaning solution containing sodium hydroxide (NaOH), with powerful cleaning and degreasing capabilities.
3. Disinfect, clean, protect
Apply directly to surfaces, water lines, irrigation systems, CIP circuits, or water treatment — depending on your application. Both outputs break down to saltwater after use.

What Makes OmniLyte's ECA Technology Unique
Our proprietary diaphragmatic cell physically separates the anode and cathode chambers, preventing the reactive streams from mixing.
This ensures the pure production of hypochlorous acid, rather than reverting to less effective compounds like sodium hypochlorite, which commonly forms in unipolar or non-separated systems.
Download our Technical Brochure below to learn more about electro-chemically activated water.
Explore Our Full Line of Electrolyzed Water Generators and Systems
-

Anolyte Generators
These industry-leading electrolyzed water machines use advanced Electrochemical Activation (ECA) technology to produce Anolyte, a non-toxic, hypochlorous (HOCl) acid-based solution that allows you to eliminate bacteria and viruses without relying on hazardous chemicals.
- Chemical free and powerful disinfection
- Low salt and low energy options
- Plug and play options for easy integration
Applications: Greenhouses, livestock operations, healthcare, food processing, drinking water systems
-

Alkalizer Systems
These advanced alkaline water systems use electrolysis to enhance water with minerals, optimize pH, and improve hydration through micro-clustering.
- Full alkaline water system
- Larger capacity
- Extra automation and control features
- Integrate instrumentation sets
Applications: Beverage industry and water bottling
-

Reverse Osmosis
Commercial reverse osmosis systems are engineered to economically produce high purity water by removing most dissolved minerals, bacteria, particles and organic impurities.
- Capacities up to 432,000 GPD
- Commercial grade components
- Options for up to 95% recovery
Applications: Light industrial, commercial, water bottling and beverage


OmniLyte Certifications

Why Partner With OmniLyte?
-
Eco-Responsibility
Our technology is designed to balance industrial productivity with environmental stewardship.
-
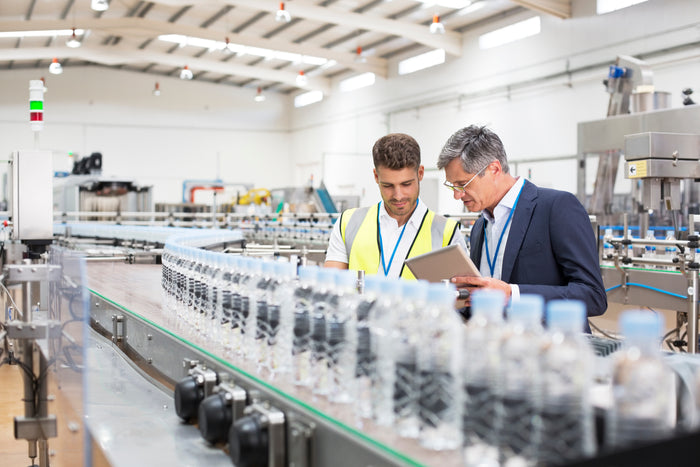
Scalability & Adaptability
We offer customizable solutions that evolve with industry needs.
-
Innovation for a Better Tomorrow
We research and develop forward-thinking technologies for a cleaner, greener future.
